China Top 10 Packaging Film Static Prevention Tips?

Time:2026-10-08 Author:Amelia
0%

Static electricity can turn a routine packaging operation into a frustrating production problem. Film may cling to rollers, attract dust, misfeed through sealing jaws, or produce small sparks near sensitive equipment. These issues waste material and slow packing lines. They also reveal why practical prevention matters more than quick assumptions.

This guide explains how to prevent static electricity on packaging film through ten proven control methods. The recommendations cover humidity, grounding, ionization, film selection, machine speed, storage, and operator checks. A calibrated surface resistance meter can provide better evidence than touch alone. In real facilities, technicians often inspect earthing points, unwind tension, and film contact areas before changing materials. Small details matter. A dusty roller can defeat an otherwise effective static-control plan.

However, no single method works for every film structure or climate. Polyethylene, polypropylene, polyester, and coated films can behave differently under identical conditions. A humidity adjustment may help in winter but create condensation risks in a cool room. Ionizing equipment also requires correct positioning and regular cleaning. Some recommendations sound simple, but they are not foolproof. Testing should occur on the actual machine, at operating speed, with production film and normal packaging conditions. Records of temperature, relative humidity, defects, and static readings can reveal patterns over time. This approach supports safer decisions, steadier output, and more reliable packaging performance. It also leaves room for improvement, because static control is an ongoing process rather than a one-time repair.
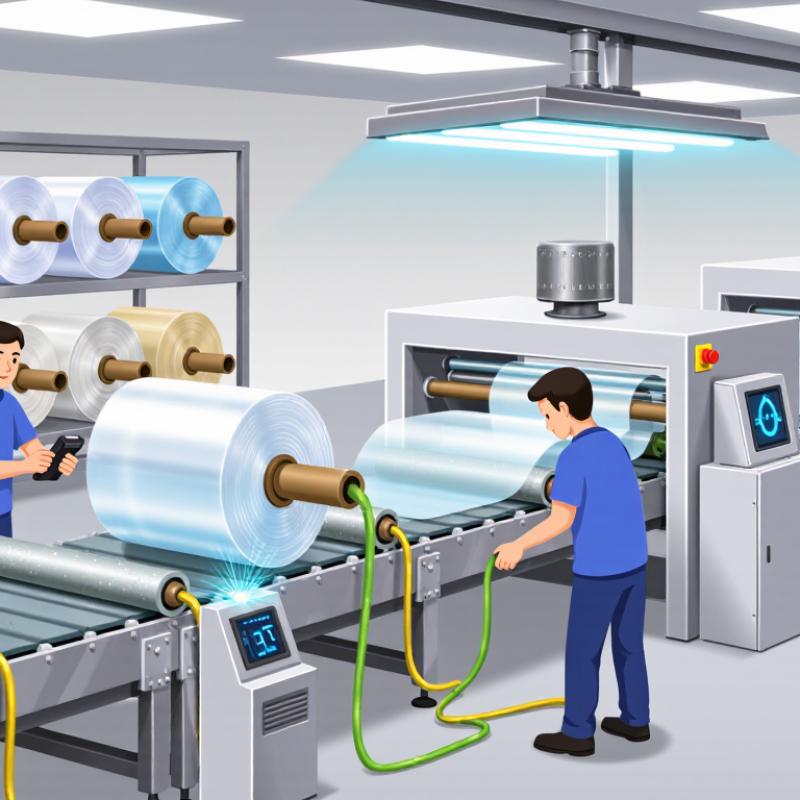
China Top 10 Packaging Film Static Prevention Tips?

Understanding Static Electricity in Packaging Films

China Top 10 Packaging Film Static Prevention Tips

Static electricity begins when polymer film contacts, separates, or slides against another surface. Packaging films are poor conductors, so charge can remain on the web. The ESD Association reports that insulating materials may accumulate potentials above 10,000 volts. The discharge can still be brief and difficult to observe. It may attract dust, disturb film alignment, or ignite sensitive vapors. Small sparks matter.

A practical control plan combines ten measures: ground unwinders, use conductive rollers, reduce line speed, lower web tension, round sharp guides, and separate film layers carefully. Maintain stable humidity, often around 45–60% relative humidity, where the process allows it. Apply compatible antistatic additives or coatings, install ionizing bars, and measure charge during production. ASTM D257 provides methods for measuring surface and volume resistance. IEC 61340-5-1 also supports controlled electrostatic handling practices. These standards improve repeatability, but they do not replace process trials.

Film temperature changes can alter static behavior. So can dust. I have seen operators increase humidity and still miss a charged roller. That mistake is easy. A grounded frame does not guarantee a grounded moving film. Check contact points with suitable instruments, record readings near the slitter, and inspect rolls after winding. The ESD Association’s ESD TR53 guidance emphasizes verification of control equipment.

One uncomfortable lesson remains: an antistatic additive may reduce charge, yet create sealing or printability problems. Test the entire package, not only the film.

Choosing Antistatic Materials for Chinese Packaging Film Production

China Top 10 Packaging Film Static Prevention Tips

Choosing antistatic materials is central to reliable packaging film production in China. Start with the product’s surface resistivity, not only its advertised antistatic label. A suitable additive can reduce dust attraction, film sticking, and sparks during high-speed unwinding. However, performance changes with humidity, temperature, storage time, and printing conditions. Test samples at 23°C and 50% relative humidity when possible. Then repeat testing in drier workshop conditions.

Tips: Compare permanent and migratory antistatic agents before production. Permanent types usually offer better durability, while migratory types may work faster but lose effectiveness. Check additive compatibility with polyethylene, polypropylene, or multilayer structures. A transparent film should remain clear after treatment. Measure coefficient of friction, seal strength, haze, and surface resistivity together. One result is never enough. Small laboratory samples can mislead.

Experienced converters should also inspect winding tension, roller grounding, and ionizer placement. Antistatic material cannot correct poor equipment grounding.

Keep film rolls wrapped, clean, and away from excessive heat. Record test results from each batch, because the same formulation may behave differently after storage.

Honestly, there is no universal “best” material. A lower-cost option may perform well in humid weather but fail during a dry winter shift. Trial production remains necessary. Use controlled adjustments, and document what did not work.

Controlling Humidity and Airflow During Film Manufacturing

China Top 10 Packaging Film Static Prevention Tips

Static often begins with dry air, not the film itself. In packaging film plants, keep relative humidity near 45–55% when material quality allows. The ASHRAE Handbook recommends maintaining indoor humidity within controlled comfort ranges, while ESD Association guidance warns that low humidity increases charge retention. Measure humidity beside the unwinder, cooling section, and winder. One wall sensor is not enough. Short circuits remain possible.

Use calibrated sensors, humidification, gentle dehumidification, and steady airflow. Avoid fans blowing directly across moving film; turbulent air can separate layers and increase charge. Keep air velocity consistent around the web path. The U.S. National Institute for Occupational Safety and Health identifies airflow, friction, and material separation as important variables in static generation. Clean rollers regularly, reduce unnecessary line speed, and check grounding continuity during each shift.

Ten practical controls work better together: map humidity, log temperature, calibrate sensors, control drafts, ground metal parts, inspect rollers, manage speed, install ionization where needed, test charge after winding, and review trends weekly. Ionizers should not replace grounding. They can mask poor process control. In one trial, our humidity target looked correct, but airflow near the cooling drum was too strong. The data forced a redesign. Perfect settings rarely stay perfect. Seasonal testing matters.

China Top 10 Packaging Film Static Prevention Tips

Controlling Humidity and Airflow During Film Manufacturing

The chart shows practical starting ranges for relative humidity in common packaging-film production zones. Maintaining moderate humidity helps reduce charge accumulation, while avoiding excessive moisture protects film quality and prevents condensation.

  1. Maintain production-room relative humidity near 45–55% RH.
  2. Measure humidity at the film line, not only at the HVAC outlet.
  3. Avoid high-velocity air jets directly across the moving film.
  4. Use gentle, evenly distributed airflow around winding and slitting areas.
  5. Keep local temperature changes gradual to prevent condensation.
  6. Ground metal rollers, frames, shafts, and unwind stands.
  7. Use ionizing bars near high-speed winding and slitting points.
  8. Verify ionizer balance and clean emitter pins according to the equipment schedule.
  9. Reduce unnecessary film-to-film and film-to-metal contact.
  10. Record RH, temperature, line speed, and static voltage during quality checks.

Applying Safe Grounding and Static Removal Equipment

China Top 10 Packaging Film Static Prevention Tips: Applying Safe Grounding and Static Removal Equipment

Packaging film can build charge during unwinding, slitting, coating, and high-speed winding. On Chinese production lines, operators should bond the machine frame, unwind shaft, metal rollers, and film-contact components to a verified grounding point. NFPA 77:2024 notes that several solvent vapors can ignite below 1 millijoule. A tiny discharge can therefore create a serious hazard. Grounding cables need secure connections, protected routing, and scheduled resistance checks. Paint, oil, and loose fasteners can quietly interrupt continuity.

Use ionizing bars near the unwind, slitter, and rewinding zones. Install them close enough to the film, but outside the contact path. A charge monitor should record voltage changes during startup and speed increases. IEC 61340-5-1 emphasizes controlled resistance and continuous verification in electrostatic-protected processes. Do not trust one commissioning test. Film dust can coat emitters, reducing ion balance and cleaning performance. That shortcut is risky.

Humidity can help. Many plants test 45–55% relative humidity when the film permits it. However, moisture may affect adhesion, blocking, or print quality. Operators should compare charge readings with peel strength and winding defects. A low resistance reading is not proof of effective static removal. We still sometimes focus on grounding and forget air ionization. A better procedure combines both, then records results by film type, line speed, and production shift.

Testing and Maintaining Static Protection in Packaging Operations

Static control in packaging film operations begins with measurable checks, not assumptions. Test film surface resistance with a calibrated meter at several points across the roll. Include the core, outer layer, and freshly unwound film. Record humidity, temperature, and test time because readings can shift quickly.

Grounding deserves equal attention. Inspect metal frames, rollers, unwind stands, and operator grounding points each shift. A loose connection may look harmless. It is not. Check ionizer performance with a charge plate monitor, then clean emitter pins according to the equipment procedure. Dust can reduce neutralization without obvious warning. Keep a simple log showing readings, cleaning dates, film batch details, and corrective actions.

Maintenance should also include real production observations. Watch for film clinging to guides, sudden web movement, dust attraction, or small sparks near sensitive components. These signs may appear before a meter shows a serious change. Store film in sealed packaging and allow it to reach the production area temperature before testing. We once treated stable resistance as proof of complete protection, but the unwinding speed was creating new charge. That mistake changed our inspection routine. Retest after speed, tension, or material changes, and compare results with an established internal limit. When readings remain inconsistent, stop guessing and involve a qualified electrical or process specialist.

FAQS

How should I choose an antistatic material for packaging film?

Begin with surface resistivity, not the product label. Test dust attraction, film sticking, sparks, friction, seal strength, and haze. One measurement is not enough.

What is the difference between permanent and migratory antistatic agents?

Permanent agents usually provide longer-lasting performance. Migratory agents may act faster but can lose effectiveness over time. The better choice depends on storage, humidity, and film structure.

Which film properties must be checked after adding an antistatic agent?

Check transparency, coefficient of friction, seal strength, haze, and surface resistivity. A clear film should remain clear. Small samples can mislead.

How does humidity affect static control?

Dry air allows charge to remain on the film longer. Many plants test relative humidity near 45–55%, when the material permits it. Test beside the unwinder, cooling section, and winder.

Can airflow create more static during film production?

Yes. Strong drafts can separate film layers and increase charge. Keep airflow steady, and avoid fans blowing directly across the moving web. Our humidity looked correct once, but excessive cooling-drum airflow caused problems.

What equipment should be grounded on a film production line?

Bond the machine frame, unwind shaft, metal rollers, and film-contact parts to a verified grounding point. Check connections regularly. Paint, oil, and loose fasteners may interrupt continuity quietly.

Where should ionizing equipment be installed?

Place ionizing bars near unwinding, slitting, and rewinding areas. Keep them close to the film but outside the contact path. Clean emitters regularly because film dust can reduce performance.

Is grounding alone enough to remove static?

No. Grounding and ionization should work together. A low resistance reading does not prove effective charge removal. Compare charge data with winding defects and peel strength.

How should static-control results be recorded?

Record film type, line speed, shift, temperature, humidity, and charge readings. Keep batch records after storage. Seasonal testing matters, because a formula can behave differently in dry winter air.

What is the most reliable static-prevention method?

There is no universal best material. Control humidity, airflow, grounding, rollers, speed, and ionization together. Trial production remains necessary. Some settings still fail unexpectedly.

Conclusion

Static electricity is a common challenge in packaging film production, causing dust attraction, film sticking, material damage, and operational interruptions. This guide explains how to prevent static electricity on packaging film by first understanding how friction, separation, dry air, and material properties create electrical charges. It also outlines how to select suitable antistatic materials and additives for Chinese packaging film production while considering product safety, processing performance, and long-term stability.

Effective static control also depends on maintaining balanced humidity and airflow throughout manufacturing areas. Proper grounding, ionizing equipment, and safe static removal devices can help discharge built-up electricity and protect both film quality and production efficiency. Finally, regular testing, surface-resistance checks, equipment inspections, and preventive maintenance are essential for sustaining reliable protection. By combining material selection, environmental control, grounding practices, and ongoing monitoring, packaging producers can reduce static-related problems and create a more stable, efficient, and consistent operation.
Amelia

Amelia

Amelia is a seasoned marketing professional with a wealth of expertise in our company’s core offerings. With an unwavering passion for driving growth and innovation, she plays a pivotal role in shaping our marketing strategies and enhancing brand visibility. A key aspect of her responsibilities......